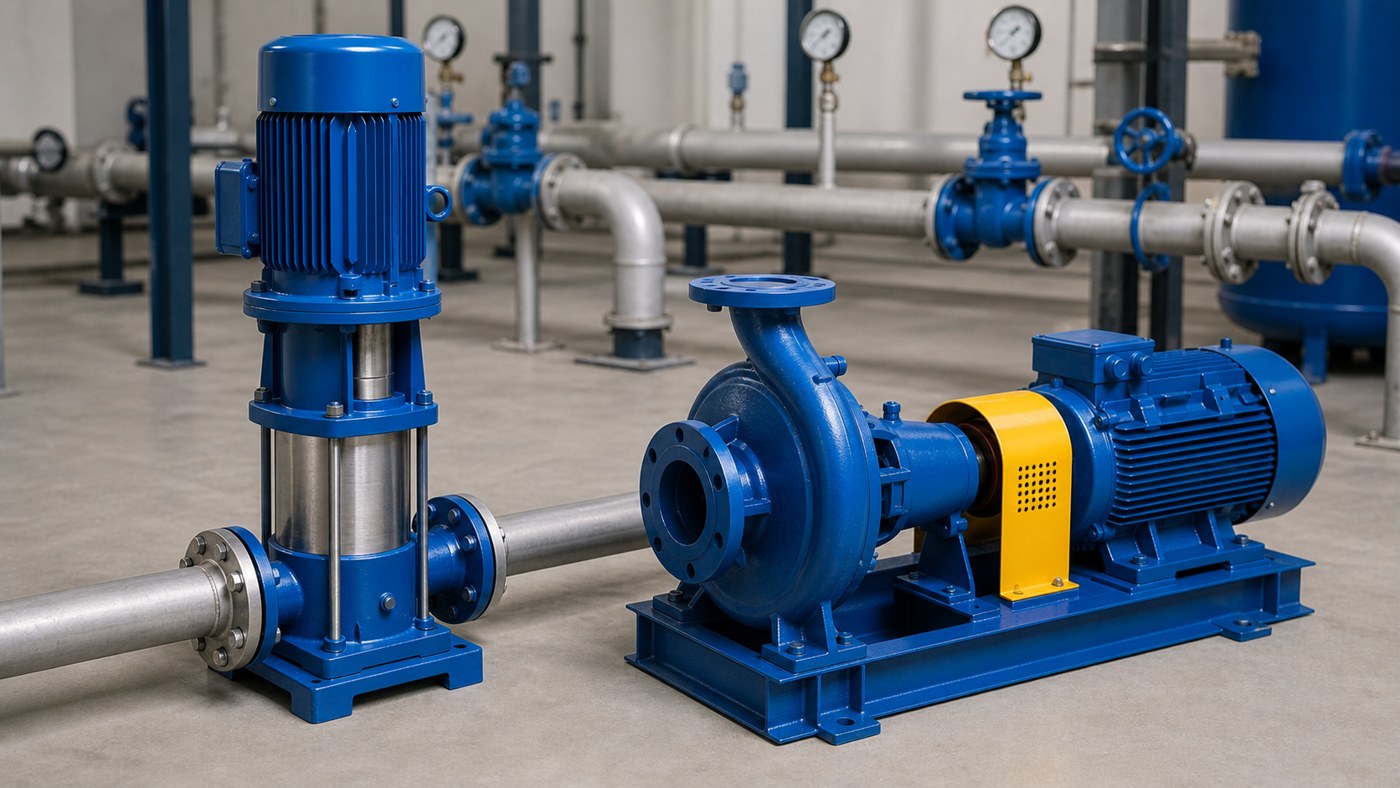
Replacing a vertical inline pump mechanical seal requires shutting down the system, isolating the pump, accessing the seal chamber from either the motor or volute side depending on the design, removing the worn seal components in the correct sequence, cleaning the seal faces and hardware, installing the new seal with proper alignment and compression, and testing for leaks under controlled startup conditions. Most inline pumps allow seal access without removing the entire pump from the pipeline, but the exact procedure depends on whether you have a cartridge seal or component seal, back-to-back or single-spring design, and whether the impeller must be removed first. This guide walks through the field procedure, the common mistakes that cause premature seal failure, and the checks that confirm the replacement will last.
Key Takeaways
- Confirm the seal type, shaft size, and seal chamber dimensions before ordering the replacement; incorrect seal selection accounts for most field installation failures.
- Always check the cause of the original seal failure—cavitation, dry running, misalignment, or chemical attack—and correct the root cause before installing the new seal.
- Cartridge seals simplify installation and reduce alignment errors, but component seals allow repair of individual parts if you have proper measurement tools and experience.
- Record shaft runout, impeller position, and coupling alignment before disassembly so you can restore the original geometry during reassembly.
- Test the seal under controlled flow and pressure before returning the pump to full duty; most leaks appear within the first few minutes if installation was incorrect.
Preparation and Safety Before Seal Replacement
Start by isolating the pump from the system. Close suction and discharge isolation valves, lock them out, and drain the pump casing through the drain plug or vent connection. For pumps handling hot, toxic, or corrosive liquids, allow time for cooling and flushing before opening the seal chamber. Verify zero pressure with a gauge or by cracking a drain valve before removing any bolts.
Record the pump nameplate data, including model, serial number, impeller diameter, and seal size. Take photos of the coupling, motor mounting, and piping arrangement so you can verify alignment and positioning during reassembly. If the pump has a spacer coupling, measure the gap between coupling hubs before disconnecting; this dimension controls axial position and affects seal compression.
Gather the replacement seal, gaskets, shaft sleeve if applicable, assembly lubricant, and the manufacturer’s installation drawing. You will also need standard hand tools, a dial indicator or feeler gauge for checking runout and alignment, a torque wrench for seal gland bolts, and clean rags. Do not reuse old gaskets, O-rings, or set screws even if they look acceptable.
Removing the Old Mechanical Seal
Vertical inline pumps typically allow seal access from the motor side after removing the motor and coupling guard. Disconnect the motor electrical supply, remove the coupling guard, and loosen the coupling fasteners. If the pump has a spacer coupling, slide the spacer toward the motor to create clearance without disturbing the pump volute or piping.
Remove the motor mounting bolts and lift the motor assembly straight up. The shaft will withdraw from the pump, exposing the seal gland and seal components. For cartridge seals, the entire seal assembly comes out with the shaft. For component seals, the rotating element stays on the shaft while the stationary seat remains in the gland.
Inspect the removed seal for the failure mode. A chipped or cracked seal face indicates solids, dry running, or thermal shock. A worn or corroded shaft sleeve suggests chemical attack or cavitation erosion. A distorted spring or stuck sliding ring points to coking, scaling, or misalignment. Document the failure mode so you can address the root cause before installing the new seal.
For component seals, remove the gland bolts and pull the gland away from the pump. The stationary seat will come out with the gland or remain in the seal chamber. Use a seal puller or carefully pry the rotating seal assembly off the shaft, noting the orientation of springs, clips, and drive collars. Clean the shaft sleeve and seal chamber with a lint-free cloth and mild solvent, checking for scoring, corrosion, or deposits that could damage the new seal faces.
Installing the New Mechanical Seal
Cartridge seal installation is faster and more reliable for most field conditions. Slide the cartridge onto the shaft until it contacts the impeller hub or shaft shoulder, following the manufacturer’s installation length dimension. Tighten the set screws or locking collar to the specified torque, apply assembly lubricant to the seal faces, and remove any shipping clips or spacers that hold the seal in the compressed position. Lower the motor and shaft assembly back into the pump, guiding the seal chamber into the gland housing, and bolt the motor in place.
Component seal installation requires more care. Install the stationary seat into the gland or seal chamber, ensuring the O-ring is seated in the groove without twists or pinches. Slide the rotating seal assembly onto the shaft sleeve with the correct spring orientation—compression springs face the liquid side on most designs. Push the rotating unit to the correct axial position, which is usually set by the impeller back face or a measurement from the shaft end, and tighten the set screws evenly to avoid cocking the seal. Install the gland over the shaft, align it with the bolt holes, and torque the gland bolts in a cross pattern to prevent distortion.
Check that the seal faces make contact without excessive compression. Too much compression overheats the faces; too little allows leakage. The installation drawing will specify the correct gap or contact pressure. For pumps with adjustable impeller clearance, verify the impeller position before final assembly, since moving the impeller changes seal compression.
Common Installation Mistakes and How to Avoid Them
- Installing the seal backward: Most mechanical seals have a specific rotation direction. The seal face with the softer material (carbon or ceramic) is usually the rotating element, while the harder face (silicon carbide or tungsten carbide) is stationary. Check the installation drawing.
- Forgetting to remove shipping clips: Cartridge seals include temporary clips or bands that hold the assembly together during shipping. If you leave these in place, the seal cannot compress properly and will leak immediately.
- Overtightening set screws: Excessive torque on set screws can crack the seal housing or damage the shaft sleeve. Use the specified torque and apply thread locker to prevent loosening.
- Reusing old gaskets or O-rings: Even if they look undamaged, old sealing elements lose compression and may not seal reliably. Replace all soft goods during seal installation.
- Skipping shaft runout and alignment checks: Excessive shaft runout or coupling misalignment causes premature seal wear. Check runout with a dial indicator; runout should be less than 0.002 inches for most seals.
- Operating the pump dry during startup: Always prime the pump and verify liquid flow before starting. Dry running destroys seal faces in seconds.
Startup and Leak Testing
After reassembly, open the suction valve slowly and vent air from the casing through the vent plug. Confirm the pump is full of liquid before starting the motor. Start the motor and immediately check for leaks at the seal gland. A few drops during the first minute is normal as the seal faces bed in, but continuous dripping indicates incorrect installation or a damaged seal.
Monitor seal chamber temperature, motor amperage, and vibration during the first 15 minutes of operation. Seal chamber temperature should stabilize within 20-30°F of liquid temperature for water service. Higher temperatures suggest dry running, cavitation, or excessive seal compression. If the motor draws more current than the nameplate rating, check for impeller binding, wrong rotation, or deadheaded discharge.
Run the pump at partial flow initially, then gradually open the discharge valve to design flow while watching for leaks, overheating, or abnormal noise. Record baseline data—suction pressure, discharge pressure, flow, amperage, and seal temperature—so you can detect changes during future operation.
When to Call a Professional
Seal replacement on standard clean-water inline pumps is within reach of most maintenance teams if you have the manufacturer’s documentation, proper tools, and alignment experience. However, call a pump service technician if the pump handles hazardous liquids, operates at high pressure or temperature, uses a complex seal arrangement like double seals with barrier fluid, or has failed repeatedly due to system problems you cannot diagnose. For fire pumps, many jurisdictions require certified technicians to perform seal work and re-test the pump to NFPA standards before returning it to service.
FAQs
Can I replace just the seal faces without buying a complete seal kit?
On component seals, you can sometimes replace only the worn faces if the springs, hardware, and O-rings are in good condition. However, most manufacturers recommend replacing the entire seal assembly to avoid mixing old and new parts with different wear patterns. For cartridge seals, face replacement is not practical in the field.
How do I know if the seal failure was caused by the pump or the system?
Inspect the seal faces and shaft sleeve. Chipping, heat cracks, or worn faces suggest system problems like cavitation, air entrainment, or dry running. Corrosion or chemical deposits indicate wrong seal materials for the liquid. Cocking or uneven wear points to misalignment or shaft runout. If the faces are clean and evenly worn, the seal likely reached its normal service life.
What is the difference between a single and double mechanical seal for inline pumps?
Single seals have one set of seal faces and allow a small amount of liquid to lubricate the faces. Double seals have two sets of faces with a barrier fluid in between, used for toxic, flammable, or abrasive liquids where any leakage is unacceptable. Double seals require a reservoir, circulation system, and pressure or temperature monitoring, so they are more complex to install and maintain.
Should I use a cartridge seal or component seal for replacement?
Cartridge seals cost more but reduce installation time and eliminate many alignment errors because all components are pre-assembled and set to the correct compression. Component seals are cheaper and allow partial replacement, but require careful measurement, proper tools, and more experience. For critical applications or if you lack a dial indicator and installation drawing, choose a cartridge seal.
How long should a mechanical seal last on a vertical inline pump?
In clean water service with proper operating conditions, a mechanical seal typically lasts 2-5 years or 15,000-30,000 hours. Seals in abrasive, corrosive, or high-temperature service may last only 6-18 months. Frequent starts, cavitation, dry running, and misalignment all shorten seal life significantly.
Conclusion
Replacing a vertical inline pump mechanical seal is a manageable field task if you understand the seal type, follow the manufacturer’s installation procedure, and address the root cause of the original failure. Always confirm shaft alignment and runout, use new gaskets and O-rings, and test the seal under controlled startup conditions before returning the pump to full duty. If the pump handles hazardous liquids, operates in fire service, or has failed repeatedly, involve a qualified pump technician who can diagnose system issues and verify compliance with applicable codes. Document your installation measurements and startup readings so future seal replacements can reference a known-good baseline.